



Supplier Inspection Procedure for Waterproof M12 Ethernet Connectors
Supplier Inspection Procedure for Waterproof M12 Ethernet Connectors
Introduction
Selecting the right M12 Ethernet connector is only the first step toward building a reliable industrial network. Before connectors are delivered to an automation, robotics, control, or Industrial Ethernet project, suppliers should carry out systematic inspections to verify electrical performance, mechanical quality, waterproof protection, and production consistency.
A professional Check M12 Ethernet Connector Procedure should therefore go beyond a simple continuity test. It should verify the connector specification, coding, dimensions, wiring, contacts, insulation, shielding, sealing system, mechanical construction, and—where required—Ethernet signal performance.
For buyers, understanding this inspection process makes it easier to evaluate an M12 Ethernet connector supplier and identify potential quality risks before mass production.
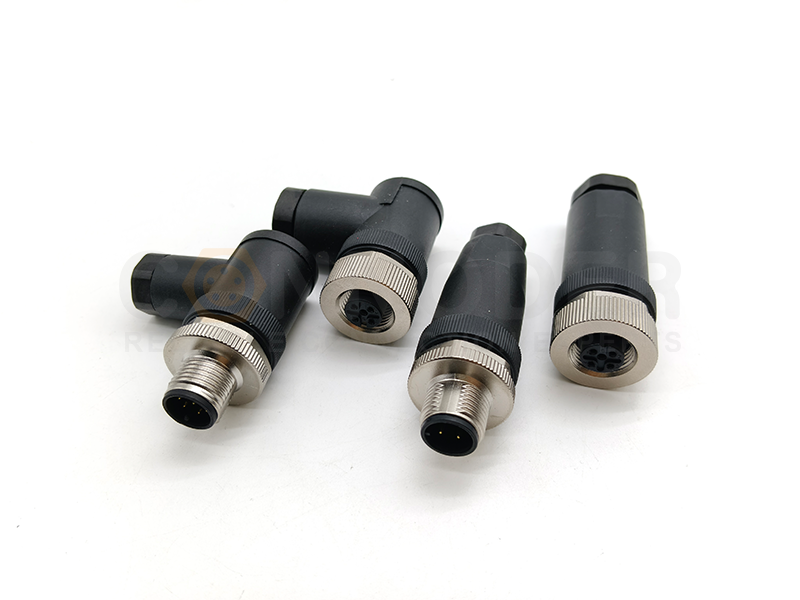
Circular Connectors
Rugged, compact and versatile — ideal when you need mixed power & signal plus environmental protection.
Why Is an M12 Ethernet Connector Inspection Procedure Important?
M12 connectors are widely used in industrial automation, robotics, sensors, control systems, machine vision, and Industrial Ethernet applications. These environments can expose connectors to vibration, moisture, dust, temperature fluctuations, mechanical stress, and electromagnetic interference.
A connector can look perfect externally and still contain an electrical or assembly defect.
For example:
Incorrect pin assignment can prevent Ethernet communication.
Poor contact quality can increase contact resistance.
Improper shielding can affect EMC performance.
Damaged seals can allow water ingress.
Poor cable termination can cause intermittent connections.
Dimensional deviations can affect mating and sealing.
Inconsistent manufacturing batches can create unexpected field failures.
This is why a structured supplier inspection procedure is important before M12 Ethernet connectors are approved for production.
Reference production‑inspection practices for M12 connectors commonly include visual, dimensional, electrical, mechanical, and environmental testing.
M12 Ethernet Connector Inspection: What Should Suppliers Check?
A complete inspection procedure can be divided into several stages:
Product specification verification
Visual inspection
Dimensional inspection
Pinout verification
Continuity testing
Contact resistance testing
Insulation and dielectric testing
Shielding inspection
Ethernet signal testing
Waterproof and environmental testing
Mechanical testing
Batch and documentation inspection
This approach gives buyers a more complete picture of connector quality than checking only whether the connector can establish an Ethernet link.
1. Verify the M12 Ethernet Connector Specification
Before testing begins, the supplier should confirm that the actual production item matches the approved product specification.
The inspection document should clearly identify:
M12 connector series
Connector coding
Number of contacts
Male or female configuration
Straight or right‑angle design
Cable specification
Contact material
Contact plating
Housing material
Shielding requirement
Ethernet performance
Operating temperature
IP protection rating
Mechanical requirements
Applicable drawings
Product revision
Check M12 Coding Carefully
M12 Ethernet connectors are available in different coding configurations.
D‑coded M12 connectors are commonly used for industrial Ethernet applications, while X‑coded M12 connectors are designed for higher‑speed Ethernet applications using four differential pairs.
The supplier should confirm the coding against the approved drawing instead of relying solely on the connector's appearance.
For a customized project, the buyer should also confirm the pin assignment before mass production.
Infographic comparing M12 D‑coded and M12 X‑coded Ethernet connectors, keying, pin configuration, cable structure, industrial applications, orange accent
2. Perform a Visual Inspection
Visual inspection is the first physical quality check.
The supplier should inspect the connector housing, contacts, cable, sealing components, and termination area.
Housing Inspection
Check for:
Cracks
Deformation
Scratches
Burrs
Surface damage
Incorrect markings
Damaged threads
Incorrect coding
Contact Inspection
Check:
Contact alignment
Pin position
Contact damage
Contamination
Surface condition
Plating consistency
Sealing Inspection
For waterproof M12 Ethernet connectors, inspect:
O‑rings
Gaskets
Sealing surfaces
Cable‑entry areas
Overmolding
Strain‑relief areas
A damaged or incorrectly positioned sealing component can compromise the connector's environmental protection.
3. Check M12 Connector Dimensions
Dimensional consistency is critical for connector interchangeability and reliable mating.
The supplier should measure the dimensions specified on the approved engineering drawing.
Typical inspection points include:
M12 thread
Connector diameter
Housing length
Pin position
Contact pitch
Keying dimensions
Cable outlet
Panel‑mount dimensions
Sealing dimensions
Why Thread Inspection Matters
The M12 threaded coupling system must mate correctly with the corresponding connector.
Thread defects can lead to:
Difficult mating
Loose connections
Insufficient sealing
Mechanical damage
Reduced vibration resistance
For high‑volume production, calibrated gauges and measurement equipment should be used according to the supplier's quality‑control procedure.
4. Verify the M12 Ethernet Pinout
Correct pin assignment is one of the most important steps in the Check M12 Ethernet Connector Procedure.
The supplier should compare the finished connector or cable assembly against the approved wiring diagram.
Check:
Pin‑to‑pin mapping
Conductor assignment
Differential pair assignment
Polarity
Connector coding
Cable termination
M12‑to‑M12 wiring
M12‑to‑RJ45 wiring when applicable
A continuity test alone is not sufficient if the conductors are connected to the wrong pins.
Why Pinout Verification Matters
An incorrectly wired Ethernet cable may:
Fail to establish a network link
Produce intermittent communication
Reduce network performance
Create troubleshooting difficulties during installation
For this reason, the wiring diagram should be treated as a controlled engineering document during supplier inspection.
5. Perform a Continuity Test
A continuity test confirms whether the intended electrical paths are complete.
Basic M12 Ethernet Continuity Test Procedure
Disconnect the connector or cable assembly from all powered equipment.
Identify the correct M12 pinout.
Set the multimeter or cable tester to the appropriate continuity function.
Test each required conductor.
Verify that every intended connection is present.
Check for unintended connections between conductors.
Record the test results.
For cable assemblies, suppliers may use automated testers to perform 100% continuity and wiring checks where required by the quality plan.
However, continuity testing only verifies basic electrical connectivity.
It does not prove that a high‑speed Ethernet connector meets all signal‑integrity requirements.
6. Check Contact Resistance and Insulation
Contact resistance should be measured against the approved connector specification.
High or unstable contact resistance can contribute to:
Signal loss
Electrical heating
Intermittent connections
Communication problems
Long‑term reliability issues
The supplier may also perform insulation resistance testing between contacts and between contacts and the connector shell where required.
For suitable product designs, dielectric withstand or Hi‑Pot testing may also be included in the electrical inspection plan.
The exact voltage, duration, and acceptance criteria should always be based on the applicable product specification and test requirements.
7. Inspect Shielding and Ethernet Signal Integrity
For shielded M12 Ethernet connectors, shielding quality is an important part of supplier inspection.
The supplier should verify:
Cable shield termination
Shield‑to‑shell connection
Contact between shield and connector body
Cable braid preparation
Shield continuity
Mechanical integrity of the shield connection
For higher‑speed Ethernet applications, additional signal‑integrity testing may be appropriate.
Depending on the connector and Ethernet specification, this can include:
Characteristic impedance
Insertion loss
Return loss
Crosstalk
Pair balance
Shielding effectiveness
This distinction is important because an M12 Ethernet connector may pass a basic continuity test while still failing a high‑frequency performance requirement.
8. Check Waterproof Performance
Waterproof protection is especially important for M12 Ethernet connectors used outdoors, in machine tools, factory automation, robotics, food‑processing equipment, and other demanding environments.
A supplier should not simply state that a connector is “waterproof.”
The actual inspection should consider:
Required IP rating
Test conditions
Mated or unmated condition
Cable diameter
Sealing material
O‑ring installation
Cable‑entry sealing
Housing assembly
Installation method
Environmental exposure
IP67 and IP68 Should Be Verified Against the Required Test Conditions
An IP rating describes protection against ingress under specified test conditions. Therefore, buyers should request the relevant test evidence and confirm that the tested configuration corresponds to the intended application.
What Should Be Checked Around the Seal?
O‑ring dimensions
O‑ring position
Seal compression
Cable jacket condition
Overmold integrity
Connector coupling
Thread engagement
Housing‑to‑seal interface
For critical applications, the supplier should conduct the specified ingress‑protection test and maintain the corresponding inspection record.
9. Perform Mechanical Reliability Tests
M12 Ethernet connectors used in industrial environments may experience repeated mating, vibration, cable pulling, and mechanical shock.
Depending on the product specification, suppliers can inspect:
Mating and unmating performance
Mating‑cycle durability
Cable retention
Pull‑out force
Thread integrity
Locking performance
Vibration resistance
Mechanical shock resistance
Strain relief
Mechanical inspection is especially important for cable assemblies because excessive stress at the connector‑to‑cable transition can eventually damage conductors or compromise sealing.
10. Check Materials and Plating
Material verification helps maintain consistency between production batches.
Depending on the connector design, suppliers may control:
Contact base material
Contact plating
Housing material
Insulator material
Shield material
O‑ring material
Cable jacket
Metal shell
Surface finish
For example, contact plating affects electrical contact behavior and corrosion resistance, while sealing material affects environmental performance.
Material certificates and supplier traceability documents can provide additional evidence during supplier qualification.
11. Establish Batch Inspection and Traceability
A single approved sample does not guarantee that every future production batch will have identical performance.
For this reason, a supplier quality system should include batch‑level inspection and traceability.
A practical workflow is:
Approved Specification → First Article → Raw Material Inspection → In‑Process Inspection → Electrical Testing → Environmental Testing → Final Inspection → Batch Approval → Shipment
Depending on the product and customer quality agreement:
Some electrical checks may be performed on 100% of finished cable assemblies.
Dimensional checks may use defined sampling plans.
Environmental or destructive tests may use periodic sampling.
Critical characteristics may require tighter inspection controls.
Each shipment should ideally be traceable to a production batch or lot.
12. What Should Buyers Request From an M12 Ethernet Connector Supplier?
When evaluating an M12 Ethernet connector supplier, buyers should consider more than unit price.
A supplier evaluation can include:
Technical Capability
M12 D‑coded products
M12 X‑coded products
Ethernet cable assemblies
Customized connectors
Cable termination
Shielded constructions
Waterproof configurations
Manufacturing Capability
Precision tooling
Metal processing
Plastic injection molding
Automated assembly
Cable assembly
Overmolding
Quality Capability
Incoming inspection
In‑process inspection
Final inspection
Electrical testing
Mechanical testing
Waterproof testing
Batch traceability
Inspection documentation
Engineering Support
Drawing review
Pinout confirmation
Cable selection
Customization
Sample development
Technical problem solving
This broader evaluation helps buyers distinguish between a supplier that simply sells connectors and a manufacturer capable of supporting a complete industrial connectivity project.
CONNODER: M12 Ethernet Connector Manufacturing and Customization
For companies sourcing industrial circular connectors, CONNODER provides a range of M12 connector solutions for industrial connectivity applications.
CONNODER's M12 portfolio includes different coding and construction options, including D‑coded and X‑coded M12 connectors, cable assemblies, assembly connectors, solder‑type configurations, and other customized solutions.
The company's manufacturing capabilities cover areas including tooling, precision stamping, injection molding, and automated assembly. According to its company information, CONNODER also carries out batch quality inspection and operates under ISO 9001 and ISO 14001 management systems.
These capabilities allow CONNODER to support customers from connector selection and customization through production and quality control.
For customers requiring a specific M12 Ethernet connector, the recommended process is to define the application requirements before production, including:
Ethernet performance
M12 coding
Pin configuration
Cable type
Shielding
IP protection
Operating temperature
Mechanical requirements
Connector dimensions
Testing requirements
Common Problems Found During M12 Ethernet Connector Inspection
Incorrect Pinout
Problem: The connector is physically correct but cannot establish reliable Ethernet communication.
Check: Compare the actual wiring with the approved pinout and perform a complete continuity test.
Poor Shield Termination
Problem: EMC or high‑frequency Ethernet performance may be affected.
Check: Inspect the shield‑to‑shell connection and perform appropriate signal or shielding tests.
Damaged O‑Ring
Problem: Water may enter the connector assembly.
Check: Inspect the sealing component and perform the required ingress‑protection test.
Poor Overmolding
Problem: The cable‑entry area may have reduced mechanical or environmental protection.
Check: Perform visual inspection and applicable mechanical/environmental validation.
Batch‑to‑Batch Variation
Problem: Previously approved samples perform differently from later production.
Check: Review material batches, production records, inspection data, and change‑control procedures.
How to Build a Reliable M12 Ethernet Connector Inspection Procedure
An effective supplier inspection system should connect engineering requirements with measurable quality criteria.
A recommended procedure is:
1. Confirm Specification
↓
2. Approve Drawing and Sample
↓
3. Inspect Raw Materials
↓
4. Inspect Production Dimensions
↓
5. Verify Pinout
↓
6. Perform Electrical Tests
↓
7. Inspect Shielding
↓
8. Verify Ethernet Performance
↓
9. Conduct Waterproof Testing
↓
10. Perform Mechanical Tests
↓
11. Review Batch Documentation
↓
12. Approve Shipment
This structured approach helps prevent quality problems from being discovered only after connectors have already been installed in expensive equipment.
Conclusion
A reliable Check M12 Ethernet Connector Procedure should evaluate the connector from multiple perspectives rather than relying on a single continuity test.
For waterproof M12 Ethernet connectors, the supplier inspection process should combine:
Specification Verification + Visual Inspection + Dimensional Inspection + Pinout Verification + Electrical Testing + Shielding Inspection + Ethernet Performance + Waterproof Testing + Mechanical Testing + Batch Traceability
For buyers, this process provides a practical framework for qualifying suppliers and reducing the risk of electrical, mechanical, waterproofing, or batch‑consistency problems.
For manufacturers, a documented inspection process demonstrates that product quality is being controlled throughout production rather than only checked at the final shipment stage.
With its M12 D‑coded and X‑coded connector solutions, industrial circular connector manufacturing capabilities, customization support, and quality‑control processes, CONNODER can support customers looking for reliable M12 Ethernet connectivity solutions for demanding industrial applications.
Why do M12 Ethernet connectors require full‑set quality inspection? Is continuity testing sufficient alone?
No. Simple continuity testing only verifies basic circuit connectivity. It cannot detect hidden issues such as abnormal contact resistance, poor shielding, waterproof failure, dimensional deviations, and gigabit‑rate signal attenuation. Full‑set quality inspection ensures long‑term stable operation in industrial environments.
What are the core differences between D‑code and X‑code M12 Ethernet connectors?
D‑code is designed for 100‑Mbps industrial Ethernet with a simple structure and broad compatibility. X‑code features four differential pairs and segmented shielding for superior crosstalk resistance, supporting up to 10G high‑speed industrial Ethernet transmission for high‑precision industrial control equipment.
What key items shall be verified for IP67 / IP68 certification of waterproof M12 connectors?
Do not rely solely on marked IP ratings. Verify actual test conditions including immersion depth, duration, cabled / uncabled status, sealing ring material, crimp sealing performance, and cable‑entry waterproof performance. Also confirm that test reports match real‑world application scenarios.
What are the most common quality risks for bulk‑purchased M12 connectors?
Major risks include wrong pin assignment, poor shielding termination, damaged sealing rings, voids in overmolding, and batch dimensional deviations. These defects frequently cause communication dropouts, water ingress into equipment, and intermittent equipment failures.
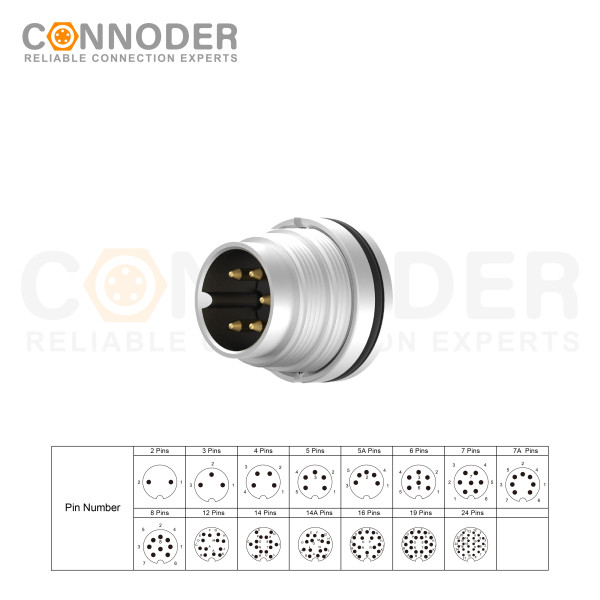
M16 6 Pin Circular Connector A-Code Interface, Waterproof Connector Receptacle Cable, Straight, Front-Locking, Unshielded
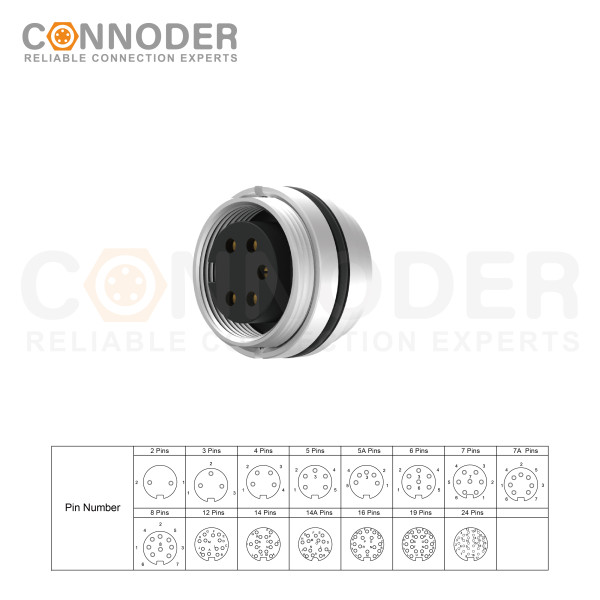
M16 6 Pin Circular Connector assemblies are ideal for demanding industrial applications such as industrial automation and aerospace, marine, and telecom systems.
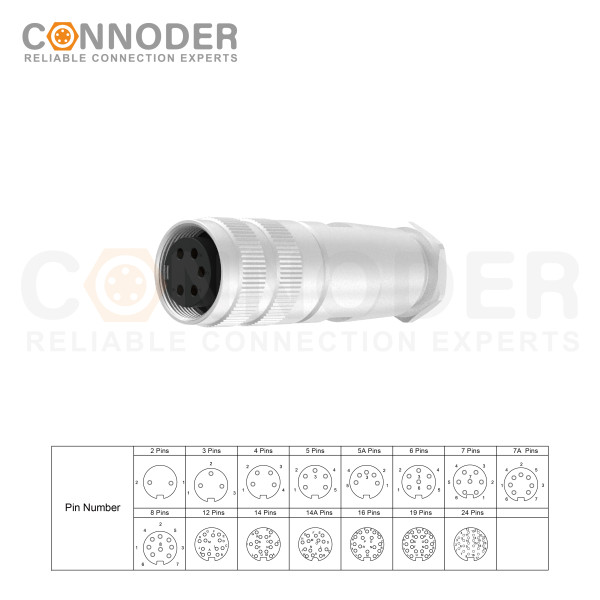
M16 6 Pin Circular Connector are ideal for demanding industrial applications such as industrial automation and aerospace, marine, and telecom systems. M16 Circular Connector are available in quick-lock wiring assembly types with IP67 protection and a vibration-resistant screw design.
M16 6 Pin Circular Connector are ideal for demanding industrial applications such as industrial automation and aerospace, marine, and telecom systems. M16 Sensor connector are available in quick-lock wiring assembly types with IP67 protection and a vibration-resistant screw design.